Complete firstClear boundary
Choose a repeatable process and product/service family; capture demand, available time, and actual work at gemba.
Without a boundary, cases, periods, or variables become mixed.
A practical method guide: clarify prerequisites and materials, understand the complete process, and look up outputs, pitfalls, and stop criteria.
What needs to be finished first
Choose a repeatable process and product/service family; capture demand, available time, and actual work at gemba.
Customer demand and available time, observed element times, layout, standardized-work combination table, WIP and quality data
What needs to be ready before start
Customer demand and available time, observed element times, layout, standardized-work combination table, WIP and quality data
Frontline operators · team lead · industrial/process engineering · safety/quality · standard owner
Choose a repeatable process and product/service family; capture demand, available time, and actual work at gemba.
90–180 minutes per repeatable work cycle plus a pilot across several cycles.
Prepare a workspace with Takt · Elements · Sequence · WIP · Confirm; separate example from live data.
The one question this method answers
Which safe, quality-capable sequence meets customer takt with the minimum required standard WIP?
Phases with goal, actions, output and pitfall
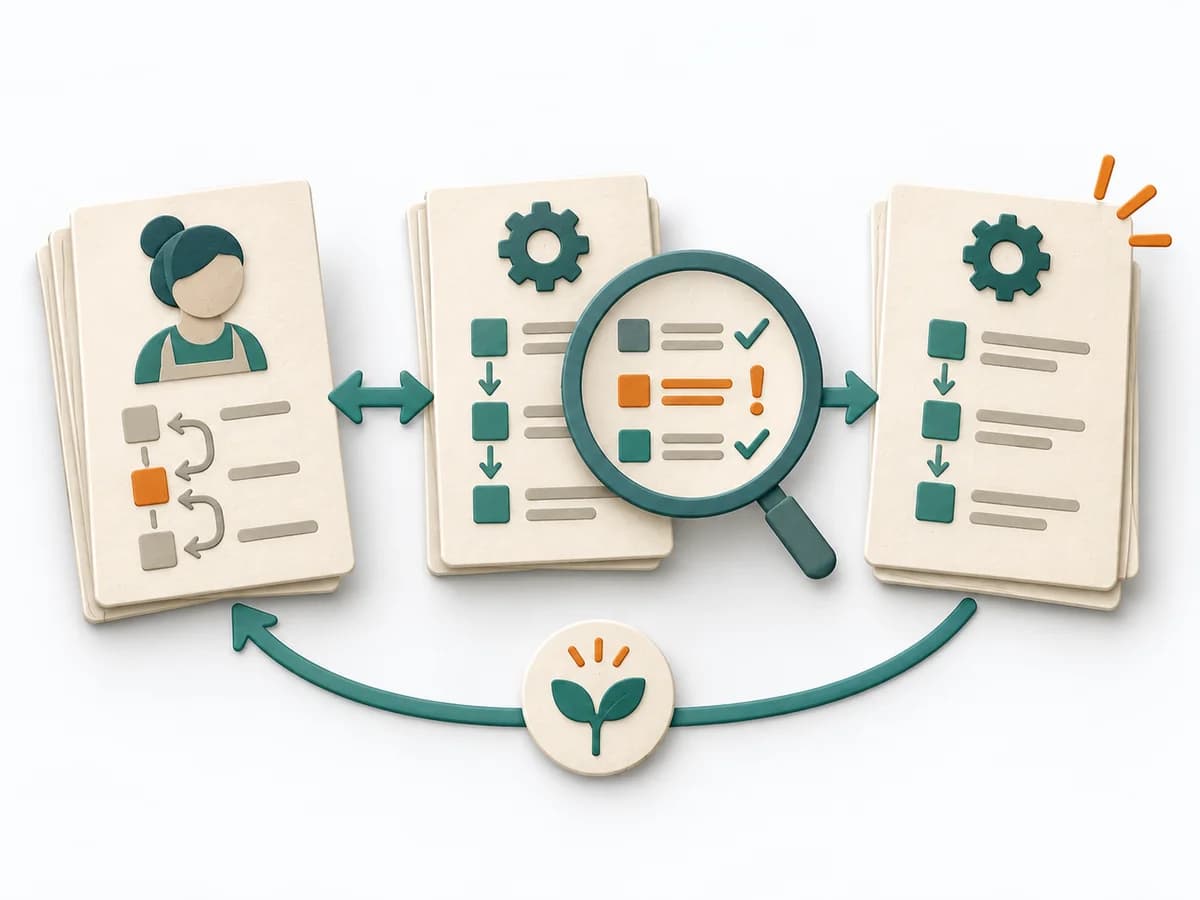
Actual work is compared with the intended standard so stable steps and variable elements become distinguishable. Deviations become signals of missing clarity or poor conditions. The improved standard supports connected training and quality work.
Fictional example
Takt: 420 net minutes / 60 units = 7.0 minutes. Manual 5.3 + walking 0.8 = 6.1 minutes; 0.6 machine minutes run in parallel.
| Sequence | Manual | Walk | Machine | Quality/Safety | Standard WIP |
|---|---|---|---|---|---|
| Scan reservationAdd evidence and rationale. | 0.6 min | 0 | 0 | ID and slot match | 1 unit in inspection |
| Fetch unitAdd evidence and rationale. | 1.8 min | 0.6 min | 0 | Lift aid above 20 kg | 8 presorted units |
| Inspect and hand offAdd evidence and rationale. | 2.9 min | 0.2 min | 0.6 min scan | Visual and function check | no extra buffer |
All values are fictional.
Takt
Goal
Takt time: Divide net available time by customer demand and set validity boundary.
Inputs for this step
Actions
Output
Takt time
Divide net available time by customer demand and set validity boundary.
Quality check
Are time base, demand, and exclusions traceable?
Pitfall
Takt is confused with observed cycle time. Calculate takt from demand and measure cycle time separately.
Timing: 15–25 minutes
Elements
Goal
Element times: Break actual work into safe observable elements and measure several cycles.
Inputs for this step
Actions
Output
Element times
Break actual work into safe observable elements and measure several cycles.
Quality check
Do times show normal variation rather than best case or estimate?
Pitfall
Management writes ideal times without operators. Involve operators and measure repeatedly under normal conditions.
Timing: 30–45 minutes
Sequence
Goal
Work sequence: Combine manual, walking, and machine time in a sensible order against takt.
Inputs for this step
Actions
Output
Work sequence
Combine manual, walking, and machine time in a sensible order against takt.
Quality check
Does sequence fit takt while retaining safety and quality steps?
Pitfall
Quality check is removed to meet takt. Remove waste, preserve mandatory controls, and assess strain.
Timing: 30–45 minutes
WIP
Goal
Standard WIP: Determine minimum standard inventory and material positions needed for stable flow.
Inputs for this step
Actions
Output
Standard WIP
Determine minimum standard inventory and material positions needed for stable flow.
Quality check
Is every WIP item justified for smooth operation?
Pitfall
Extra inventory hides variation and search problems. State the purpose of each item in process and remove unnecessary buffers.
Timing: 20–30 minutes
Confirm
Goal
Confirmed standard: Pilot standard with operators, measure deviations, display it, and establish review.
Inputs for this step
Actions
Output
Confirmed standard
Pilot standard with operators, measure deviations, display it, and establish review.
Quality check
Can several people reproduce takt, quality, and safety?
Pitfall
Standard is rolled out as immutable instruction. Label it best current method and define deviation and kaizen path.
Timing: One to three operating cycles
What comes out at the end
Sketch: what the artifact looks like
Standardized work with takt time, work sequence, manual/machine/walk time, standard WIP, layout, and review.
Record date, owner, source state, and review date; preserve prior versions.
Set subject, evidence, roles, flow, and review.
To be confirmed
To be confirmed
Complete run Time: 90–180 minutes per repeatable work cycle plus a pilot across several cycles.
Complete this worksheet on paper or in your own document during the work.
| Sequence | Manual | Walk | Machine | Quality/Safety | Standard WIP |
|---|---|---|---|---|---|
| Scan reservation | |||||
| Fetch unit | |||||
| Inspect and hand off |
The blank worksheet contains prompts only.
Reference · original teaching example
Expected artifact: Takt time
Divide net available time by customer demand and set validity boundary.
Entry:
...
Expected artifact: Element times
Break actual work into safe observable elements and measure several cycles.
Entry:
...
Expected artifact: Work sequence
Combine manual, walking, and machine time in a sensible order against takt.
Entry:
...
Expected artifact: Standard WIP
Determine minimum standard inventory and material positions needed for stable flow.
Entry:
...
Expected artifact: Confirmed standard
Pilot standard with operators, measure deviations, display it, and establish review.
Entry:
...
...
Method guide: https://methodatlas.meierhoff-systems.de/en/methods/standard-work-analysis/run-sheet
Concrete filled scenario, fictional example
Fictional example for orientation. Counts and timings describe this case and are not universal requirements.
Concrete filled scenario, fictional example
Takt: 420 net minutes / 60 units = 7.0 minutes. Sequence: 5.3 manual + 0.8 walking = 6.1 minutes; 0.6 scan machine minutes run in parallel.
| Sequence | Manual | Walk | Machine | Quality/Safety | Standard WIP |
|---|---|---|---|---|---|
| Scan reservation | 0.6 min | 0 | 0 | ID and slot match | 1 unit in inspection |
| Fetch unit | 1.8 min | 0.6 min | 0 | Lift aid above 20 kg | 8 presorted units |
| Inspect and hand off | 2.9 min | 0.2 min | 0.6 min scan | Visual and function check | no extra buffer |
Recognize symptoms and steer against them
Quick overview, the full text is in the matching phase in the flow
Takt is confused with observed cycle time.
Calculate takt from demand and measure cycle time separately.
Management writes ideal times without operators.
Involve operators and measure repeatedly under normal conditions.
Quality check is removed to meet takt.
Remove waste, preserve mandatory controls, and assess strain.
Extra inventory hides variation and search problems.
State the purpose of each item in process and remove unnecessary buffers.
Standard is rolled out as immutable instruction.
Label it best current method and define deviation and kaizen path.
When to pause, resolve prerequisites, or choose another approach
Go to the profile for purpose, similar methods, and sources or continue to the next method in the catalog.